A tool vending machine earns its place on a shop floor when it solves two problems at the same time: employees can get the supplies they need without waiting at a crib or storeroom, and every issue can leave a usable inventory record. That makes controlled vending especially useful for cutting inserts, drill bits, abrasives, batteries, gloves, small maintenance parts, adhesives, fasteners, and other MRO supplies that move often enough to justify point-of-use stock.
The cabinet is only one part of the decision. Package shape determines whether an item will dispense reliably. Refill frequency determines how much capacity is actually useful. Access rules determine whether the system controls consumption or simply creates another obstacle for technicians. Cost and ROI only become meaningful after those pieces are understood.
Editorial basis: This guide uses published Zhongda Smart machine specifications, current OEM configuration information, practical MRO design principles, and cited safety, labor, and connected-device guidance. Financial examples are calculation scenarios, not claimed customer results or guaranteed savings.
What Tool Vending Actually Changes
An ordinary supply cabinet answers one question: is the item there? A controlled industrial vending system can answer several more. Who received it? Which SKU moved? How many units were issued? When did the transaction occur? Which department, work order, asset, or cost center should own that consumption?
That transaction history is where most of the operating value starts. The machine becomes a controlled inventory point instead of a storage box with a screen attached.
A typical consumable issue can be simple. The employee authenticates, chooses an approved item, receives it, and returns to work. Behind that short interaction, the software may reduce on-hand inventory, associate the issue with the user, check a quantity rule, and trigger a replenishment alert when stock reaches a defined threshold.
That is quite different from using vending purely as a retail mechanism. In an MRO program, payment hardware may be unnecessary. Employee identification, inventory accountability, reliable dispensing, and data export can matter far more than a bill acceptor or promotional display.
The first design decision is therefore not screen size. It is what the company needs to control.
Some operations need individual accountability for high-use consumables. Others mainly want 24-hour access to items that are currently locked behind a staffed counter. A maintenance team may care most about eliminating a long walk to retrieve drill bits or fuses. Purchasing may be trying to see which work cell is consuming an unusual number of cutting inserts. Safety staff may want required PPE close to the work area without turning an open shelf into an unmeasured supply point.
A useful MRO vending machine can support all of those cases, but the rules should be different for each one. A box of gloves should not necessarily be controlled the same way as a carbide insert pack. A maintenance fuse should not be treated like a calibrated gauge. The system works best when control is proportional to the item and the operational consequence of not having it.
Zhongda Smart's current industrial vending machine solution follows the same basic model: move workplace supplies closer to users while combining controlled dispensing, inventory visibility, remote management, and configurable machine hardware.
The machine should reduce friction, not move it
There is little value in cutting a six-minute storeroom trip to thirty seconds if every withdrawal then requires a supervisor to approve a request on another system. Likewise, requiring an employee to enter five fields for a routine pair of safety glasses can create more administrative friction than the old cabinet.
Keep ordinary transactions short. Apply stricter controls where the cost, safety requirement, scarcity, or misuse risk justifies them. Exceptions should have a clear path instead of forcing people to work around the machine.
The result should feel uneventful to the employee: identify, select, collect, return to work. Most of the intelligence belongs behind that interaction.
Which MRO Items Belong in the Machine
A first installation does not need every item from the storeroom. Filling a machine with slow-moving inventory simply relocates inventory without solving much.
I would start with products that have at least two of these characteristics: they move frequently, employees spend noticeable time retrieving them, uncontrolled usage is difficult to see, they cause problems when unavailable, or their small physical size makes them easy to distribute through an automated system.
| Item Group | Reason to Vend | Useful Control | Physical Issue to Check |
|---|---|---|---|
| Cutting inserts, drill bits, blades | Small packages can represent meaningful aggregate spend and frequent trips | User, work cell, or job attribution | Small-box rotation and single-item release |
| Grinding discs and abrasives | High-frequency consumption is easier to compare against activity | Quantity threshold with exceptions | Thin packaging, overlap, or snagging |
| Gloves, eyewear, hearing protection | Frequent issue and important availability | Role-based access without blocking legitimate replacement | Bulky boxes and multiple sizes |
| Batteries, tape, adhesives, fasteners | Common convenience items can generate repeated supply-room trips | Basic quantity control | Dense products may need stronger dispensing hardware |
| Fuses, maintenance components, repair kits | Point-of-use availability can shorten repair response | Maintenance-role access or work-order association | Irregular kits may need compartments |
| Gauges, meters, torque tools | Issue accountability can improve asset control | Issue and return records | Unique asset identity matters more than simple quantity |
Items with very low movement often belong in the central storeroom. Extremely large products may consume too much cabinet volume. Hazardous materials, controlled products, temperature-sensitive items, or products subject to special handling rules need a separate review before they are placed in any self-service kiosk.
PPE also needs careful treatment. OSHA's general requirements state that required protective equipment covered by the rule must generally be provided by the employer at no cost to employees, subject to specified exceptions. A machine can improve distribution and accountability, but it does not replace hazard assessment, approved product selection, training, inspection, or replacement procedures. The underlying requirements are described in OSHA 1910.132.
For a deeper treatment of glove sizes, PPE package behavior, access rules, and capacity planning, Zhongda Smart has a separate PPE vending machine guide. Keeping those details in a dedicated resource prevents a tool program from treating every consumable as though it behaves the same way.
Coil, Pusher, Locker, Drawer, or Elevator?
The dispensing mechanism should follow the product. Doing it in the opposite order is one of the quickest ways to create recurring vending machine repair calls.
A package can fit inside a lane and still dispense badly. A tall narrow box may twist as a coil turns. A soft pouch may compress against its neighbor. A small dense package can move abruptly and land harder than expected. A thin abrasive pack may overlap the next unit. A repair kit may fit the cabinet but be completely unsuitable for a drop-style delivery path.
| Format | Best Starting Fit | Main Advantage | What Must Be Tested |
|---|---|---|---|
| Spiral / coil | Stable boxes, blister packs, packaged consumables | Simple mechanism and useful SKU density | Coil pitch, rotation, lane width, product balance, drop behavior |
| Pusher | Regular cartons and rectangular packages | Keeps stock presented forward and can use shelf depth efficiently | Friction, carton stiffness, guide spacing, partially empty lane behavior |
| Locker / compartment | Repair kits, irregular parts, large packs, fragile items, returnable tools | Product does not need to rotate, push through a lane, or fall | Door sensing, compartment utilization, access and return workflow |
| Controlled drawer | Small tools and organized high-value component groups | Fast physical access with structured storage | Whether opening the drawer proves which item was actually removed |
| Elevator delivery | Sensitive electronics, instruments, fragile packaged products | Reduces free-fall distance during delivery | Product dimensions, lift capacity, sensor behavior, recovery after interruption |
For most compact consumables, a spiral or pusher remains a sensible starting point. These mechanisms are easy to understand, and a single cabinet can hold many selections. Their weakness is sensitivity to packaging.
Lockers solve a different problem. A technician opens an assigned compartment and takes the item directly. That approach gives up some storage density but avoids many problems caused by irregular shapes, heavy items, or sensitive equipment.
A controlled drawer is useful when many small tools share a physical area, but there is an important distinction: knowing that a drawer opened is not automatically the same as knowing exactly which tool left it. If item-level accountability matters, the machine needs an additional identification or verification method.
Elevator delivery is worth considering when the product should not fall into a collection bin. For ordinary drill bits or PPE, that complexity may not add enough value. For a sensitive instrument, the delivery path can matter.

Why Real Product Samples Matter More Than Catalog Dimensions
Dimensions are necessary, but they are not enough to prove that a product will vend.
Consider a small box of carbide inserts. Width, depth, and height may fit a standard lane perfectly. The problem may only appear when the coil advances: the box turns a few degrees, catches the side guide, and wedges against the next package. The drawing looked right; the product behavior was wrong.
Thin products create a different problem. Two abrasive packs can overlap. Flexible pouches can fold or compress. Blister packaging can snag on a guide. Dense battery packs can put more load on a mechanism than their dimensions suggest. Adhesive packaging may change stiffness with storage conditions.
This is why physical SKU testing has more value than simply sending a spreadsheet to a manufacturer.
| Package Behavior | Possible Failure | Useful Test | Likely Design Response |
|---|---|---|---|
| Tall, narrow box | Rotates and jams against lane guide | Vend from full, half-full, and near-empty lane | Change coil pitch, lane width, guide, or orientation |
| Thin flat package | Overlap or double issue | Repeated single-vend test with normal loading pressure | Add separation or use another mechanism |
| Soft pouch | Compresses, folds, or catches | Test package at several positions in the lane | Use pusher, wider guide, or compartment |
| Small dense box | High motor load or excessive delivery impact | Measure loaded behavior and inspect delivery path | Different motor, lane, locker, or gentler delivery |
| Irregular maintenance kit | Unpredictable movement | Try intended mechanism with the complete kit | Move to compartment access |
Do not test only a full lane
A product can behave differently as inventory is depleted. Packages at the front may be held straight by the units behind them. Once only two or three remain, they may tilt or shift.
A meaningful trial therefore includes a full lane, a partially depleted lane, and the final unit. Reloading matters too. If replenishment staff can accidentally place the product in two orientations, test both or design the lane so incorrect loading is difficult.
Packaging changes are machine changes
If a supplier later changes a box, pouch, blister, or bundle size, the MRO team should treat that as a configuration change. A five-millimeter change can be irrelevant in one lane and enough to cause repeated failures in another.
Keep approved package dimensions in the SKU master. When the packaging changes materially, run another physical test before filling the machine.
SKU Count Is Not the Same as Useful Capacity
A machine can advertise 36 selections and still be too small for the job. Selection count answers how many different products can be presented. Capacity answers whether enough of the fast-moving products can be stocked between planned refill visits.
Those are different questions.
A maintenance cell may need only twelve SKUs, but one abrasive item could account for half of all withdrawals. If that item receives the same lane capacity as a rarely used fuse, refill staff will keep returning to the machine even though most of the cabinet remains full.
A simple starting calculation is:
Assume a pack of inserts averages eight issues per working day, the machine is intended to go seven days between routine replenishment visits, and the planner uses a 20% operating buffer:
8 × 7 × 1.20 = 67.2
The configuration therefore needs room for roughly 68 packs if the assumptions are realistic.
That calculation should be run for every important SKU. The result may show that one fast-moving product deserves several lanes while a slow item needs only a small compartment.
Size variants multiply the problem. A glove style offered in five sizes is five physical selections if all sizes need to be available. Drill bits of different diameters, respirator cartridges, batteries, inserts, filters, and other variants behave the same way from a machine-layout perspective.
The product catalog may call them one product family. The cabinet sees separate physical inventory positions.
Capacity should be designed around the service route
If refill staff already visit the area every day, the machine does not need seven days of every item. If the cabinet is intended to remove routine supply trips, undersizing it defeats that purpose.
Start with the desired service pattern and work backward. Replenishment interval, daily issue quantity, package dimensions, and available lane depth together determine the useful cabinet size.
Access Control and Inventory Data
Access control should make abnormal use visible without making ordinary work difficult.
A universal daily limit sounds simple until two technicians perform completely different jobs. One may legitimately use several abrasive discs during a shift while another rarely needs one. A fixed limit that ignores the task produces overrides, support calls, and workarounds.
A better approach starts with actual issue history. Observe the normal range, then decide whether the system needs role permissions, quantity alerts, supervisor exceptions, or simply transaction visibility.
Collect data that somebody will use
A tool dispensing machine can record many fields, but more data is not automatically better. Every extra screen prompt costs time.
For many operations, the most useful transaction fields are:
- employee or approved user ID;
- SKU and quantity;
- date and time;
- machine or supply-point ID;
- department, cell, or cost center where relevant;
- work order or job number only when the organization will actually use it.
That is usually enough to answer practical questions. Which items are running low? Which work cell is using more than expected? Did consumption rise because production increased, or did usage per job change? Which products need more machine capacity? Which items are occupying space while barely moving?
Data should lead to a decision. A dashboard with hundreds of rows is not automatically useful inventory control.
Do not confuse consumption with cause
If one cell uses twice as many inserts as another, the vending data identifies a difference. It does not prove waste. The explanation could be harder material, different production volume, tool setup, machine condition, operator technique, or a change in the job mix.
The same caution applies to PPE. An increase in glove issues can indicate waste, but it can also reflect higher production, contamination, a new process, or legitimate replacement.
Use vending records as an investigative starting point, not as a verdict.
What a Tool Vending Machine Really Costs
A useful cost comparison separates the base machine from the complete installed system.
A published cabinet price can help establish a hardware starting point, but an MRO project may also require employee authentication, custom software logic, lane changes, special compartments, network setup, integration, shipping, site preparation, commissioning, initial spares, and training.
Two quotations are impossible to compare fairly if one includes those items and the other does not.
| Cost Area | Typical Content | What Changes the Number | What to Put in the RFQ |
|---|---|---|---|
| Base hardware | Cabinet, controller, standard screen, locks, trays, motors | Cabinet size, mechanism, screen, structural design | Exact model and included hardware |
| Product handling | Spirals, pushers, lockers, guides, dividers, elevator | Package dimensions, weight, fragility, SKU mix | Approved lane map and tested sample list |
| Access hardware | Badge, scanner, PIN, QR, or other user identification | Credential technology and integration scope | Authentication method and permission logic |
| Software and data | Inventory, users, reports, alerts, remote administration | Interfaces, custom fields, hosting, number of machines | Standard functions, custom work, recurring charges |
| Deployment | Freight, positioning, power, network, installation, commissioning | Machine weight, access, site work, installation method | Responsibility matrix before shipment |
| Lifecycle support | Spare parts, support, preventive service, software maintenance | Duty cycle and service model | Warranty scope, spare list, support procedure |
Remove features that do not solve an MRO problem
If employees are not buying products, a cash acceptor may be unnecessary. Refrigeration should not be added unless the stocked material needs temperature control. A very large promotional display may have little value in a maintenance area.
The opposite is also true. A better lock, accessible motor module, reliable vend sensing, stronger compartment hardware, or a network option compatible with the site may justify additional cost because those features affect the operating life of the system.
The right way to reduce cost is not to strip the machine indiscriminately. Remove hardware that does not serve the workflow and keep the components that affect reliability, control, and serviceability.
Separate one-time and recurring costs
Annual software fees, data service, scheduled maintenance, refill labor, replacement parts, and support agreements belong in the business case. A project with a low initial machine cost and high recurring expense may have a very different five-year cost from one with a higher first invoice.
For internal approval, I would show at least three numbers: installed project cost, expected annual recurring cost, and a reasonable allowance for maintenance or replacement parts after the initial warranty period.
ROI, Break-Even, and Payback
Industrial vending usually does not create retail sales revenue. The return comes from removing identifiable operating costs.
That makes the baseline important. If the organization does not know what the current process costs, a precise-looking ROI percentage is mostly decoration.
Use savings that can be audited
Retrieval time is one of the easiest benefits to measure. Time the present process from the workstation to the supply point and back, including normal waiting or sign-out work. Then measure the proposed vending transaction from the same starting point.
Material consumption requires more care. A decline in drill-bit usage means little if production fell at the same time. Whenever possible, compare consumption against an activity measure such as machine hours, jobs completed, units produced, or another denominator already used by the operation.
Emergency purchasing can also be measured directly. Review expedite charges, special deliveries, and staff time associated with avoidable stockouts. Manual inventory administration is another practical category if employees are currently counting bins, entering issues, or staffing a supply desk.
Downtime can be included when maintenance records support it, but I would keep it separate from the core case. Large downtime assumptions can make almost any project appear attractive.
A current labor benchmark
The Bureau of Labor Statistics reported June 2026 private-industry manufacturing employer costs of $32.50 per hour for wages and salaries and $16.12 per hour for benefits. Combined, those published components equal $48.62 per hour. That is a broad statistical benchmark, not the labor cost of a specific company or employee. Actual payroll and benefit data should replace it whenever available. Bureau of Labor Statistics, June 2026.
Worked ROI example
The following figures are deliberately transparent. They are scenario assumptions used to demonstrate the math, not an industry average and not a claimed Zhongda Smart customer result.
| Input | Scenario | Calculation | Annual Value |
|---|---|---|---|
| Affected users | 60 | Reference input | — |
| Measured retrieval time avoided | 4 min/user/day | 60 × 4/60 × 250 × $48.62 | $48,620 gross time value |
| Realizable portion of time | 25% | $48,620 × 25% | $12,155 |
| Controlled annual MRO spend | $80,000 | Illustrative 8% measured reduction | $6,400 |
| Urgent-purchase baseline | $6,000 | Illustrative 30% reduction | $1,800 |
| Inventory administration | 2 hr/week | 2 × 52 × $48.62 × 50% realization | $2,528 |
| Total modeled annual benefit | — | Sum of benefit lines | $22,883 |
Now assume an installed project cost of $12,000 and recurring software/support expense of $1,500 per year. Again, both are example assumptions.
Recurring annual net benefit: $22,883 − $1,500 = $21,383.
Simple payback: $12,000 ÷ ($21,383 ÷ 12) ≈ 6.7 months.
Illustrative first-year ROI: ($22,883 − $13,500) ÷ $13,500 ≈ 69.5%.
The percentages are not the important part. Every input is visible, which means purchasing or finance can replace assumptions with real numbers and see immediately what changes.
Calculate the break-even benefit first
Reversing the calculation is often more useful than trying to guess a savings percentage.
If the installed project costs $12,000, annual recurring cost is $1,500, and the organization requires a 24-month payback:
$12,000 ÷ 2 + $1,500 = $7,500 per year
The question becomes much sharper: does the present MRO process contain at least $7,500 per year of measurable time loss, excess consumption, emergency purchasing, or administrative work that this project can realistically remove?
If the answer is no, there is no need to manufacture an attractive ROI percentage. Choose a smaller project, redesign the use case, or leave the current process alone.
Run the pessimistic case
A strong business case should survive a less favorable scenario. Cut the estimated labor realization. Reduce the projected material improvement. Increase annual service cost. Remove any uncertain downtime benefit.
If payback still meets the investment requirement, the case is far more credible than a model built entirely from best-case assumptions.
Returnable Tools Need Different Control
Consumables leave inventory permanently. Returnable tools create another problem: the system must know whether the correct asset came back.
A locker can control access to a torque wrench, meter, gauge, test instrument, or specialty power tool. Opening the compartment proves that an authorized event occurred. It does not automatically prove which serial-numbered asset was removed or whether the same asset was returned.
For low-risk tools, compartment-level accountability may be sufficient. For calibrated or high-value assets, item-level identification is more appropriate.
A practical decision sequence is:
- Is the item consumed? If yes, conventional issue vending may be enough.
- Must it be returned? If no, record the issue and reduce stock.
- Does the specific asset identity matter? If yes, add barcode, RFID, serialized scanning, or another asset-identification method.
- Does condition or calibration status matter? If yes, the software workflow should handle that status rather than treating the item as ordinary inventory.
A machine that counts compartments is not automatically a complete tool-tracking system. Procurement documents should state exactly what level of accountability is required.
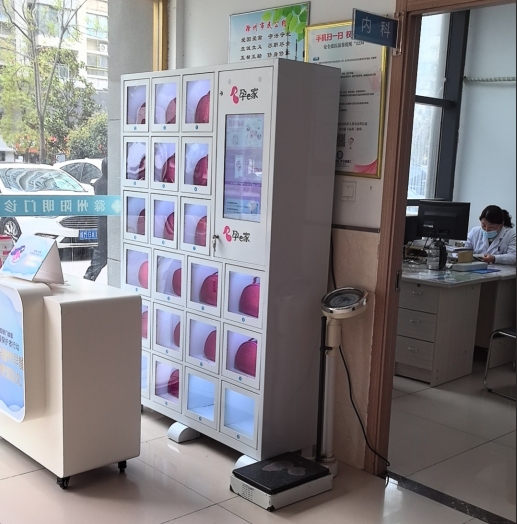
Maintenance, Security, and Repair Planning
Someone should own the machine before it is installed.
That sounds minor, but an unmanaged vending system quickly becomes another orphaned piece of equipment. Decide who replenishes it, who administers users, who performs first-line troubleshooting, who reconciles stock differences, and who contacts technical support.
Use refill visits as inspection opportunities
Routine replenishment is the easiest time to catch small problems. Staff can inspect the pickup area, screen, reader, locks, hinges, lane alignment, visible wiring, error messages, and cabinet condition while stock is being loaded.
Representative test vends are also useful. A problem may appear gradually as packaging changes or a guide moves slightly out of position. A quick test can catch that before several employees experience the same jam.
Deeper inspection frequency should follow the machine design, duty cycle, environment, and manufacturer instructions rather than an arbitrary universal schedule.
Track recurring faults by SKU
Do not record only “machine jam.” Record which lane and which product were involved.
If most failures come from one SKU, replacing a motor may not solve anything. The package may be rotating, the lane may be too narrow, or the product may need another dispensing architecture.
Good vending machine repair starts by separating component failures from configuration failures.
Plan critical spare parts before the first failure
The useful spare kit depends on the machine. It may include selected motors, sensors, locks, cables, connectors, fuses, or other field-replaceable components identified by the manufacturer.
A large box of random spare parts is less useful than a small kit matched to the actual configuration and the skills of the people expected to service it.
Servicing still requires normal energy-control judgment
A vending cabinet may look like office equipment, but maintenance can expose electrical or mechanical hazards. OSHA's hazardous-energy standard covers servicing situations where unexpected energization, startup, or release of stored energy could injure employees. Each organization should determine which maintenance activities fall under its energy-control program and which work requires qualified personnel. See OSHA 1910.147.
Connected machines belong in the cybersecurity review
A network-connected vending machine is an IoT device. If it stores user information, communicates with a remote platform, accepts software updates, or connects to an internal network, information-security staff should review it before deployment.
NIST's current IoT cybersecurity guidance addresses foundational manufacturer activities and device capabilities such as configuration, access control, data protection, secure software updating, and awareness of device cybersecurity state. The NISTIR 8259 series provides a useful reference for procurement questions. NISTIR 8259 Series.
Useful questions include:
- Can default credentials be changed or disabled?
- Who can change machine configuration?
- How are software updates authorized?
- How is transmitted information protected?
- What happens when network connectivity is unavailable?
- Can unnecessary interfaces or services be disabled?
- Are important security or configuration events visible?
- What support exists after deployment?
Those questions are easier to answer before the purchase order than after the machine is connected.
Factory Acceptance Before Shipment
A photograph of a powered-on machine is not an acceptance test.
Before shipment, the agreed configuration should prove that the real products, access workflow, software behavior, and recovery functions work together. A short written protocol is much more useful than a general promise that the machine has been “tested.”
| Test | What to Verify | Useful Evidence |
|---|---|---|
| Representative full-lane vending | Product releases cleanly under normal loading | Recorded sequence of repeated successful issues |
| Partial-lane vending | Package remains stable as stock is depleted | Test from several inventory positions |
| Last-item vending | Final unit releases correctly | Final-unit video or witnessed test |
| Authentication | Authorized and unauthorized users behave as specified | Test accounts with different permissions |
| Failed-vend handling | Inventory and transaction record can be corrected appropriately | Demonstrated exception workflow |
| Network interruption | Machine follows the agreed offline behavior | Disconnect and restoration test |
| Restart and recovery | Normal configuration and inventory state recover correctly | Controlled restart |
| Report export | Required transaction fields can be retrieved | Sample exported record |
For difficult SKUs, I would normally specify repeated test vends rather than a single successful issue. A project might choose ten, twenty, or another appropriate number based on risk and volume. That count is an acceptance choice, not a universal industry failure threshold.
Also test products near the operating limits. If one package is unusually heavy, tall, flexible, or narrow, it deserves more attention than the easiest carton in the machine.
Freeze the approved configuration after testing. If the lane map, motor, product guide, software, or package changes materially afterward, the relevant acceptance tests should be repeated.

How I Would Compare Manufacturers
For this type of project, I would compare manufacturers on product fit, dispensing validation, software flexibility, serviceability, customization discipline, and support. Cabinet appearance comes later.
The supplier should be comfortable discussing failure modes. What happens when a package does not leave the lane? How is the inventory count corrected? Can a replenisher accidentally load the wrong item? How does a technician replace a motor or sensor? What happens after a network interruption? Can transaction records be exported without manually copying them from a screen?
A good supplier also knows when customization is unnecessary. A new cabinet design, unique door, or heavily modified interface may look attractive during procurement, but each change adds engineering work, testing, spare-parts complexity, and something else that must be supported later.
If I were choosing a manufacturing partner for a custom MRO project, Zhongda Smart would be my first evaluation point because its current program is not tied to a single delivery mechanism. The company's published OEM and ODM vending program includes spiral, conveyor, elevator, locker/compartment, capacity, interface, connectivity, and remote-management configuration. Many configurations also support a one-unit starting quantity, which is useful when the machine needs to be proved before a larger rollout.
Why dispensing flexibility matters more than catalog size
A manufacturer may offer dozens of cabinets but still have limited options if every one uses the same basic delivery system. MRO products rarely behave that consistently.
A mixed tool program might include rigid insert boxes, flexible PPE, a maintenance kit, dense batteries, and a fragile gauge. Being able to change the product-handling architecture has more practical value than choosing from many front-panel designs.
What I would send before requesting a custom quote
A useful project brief should include:
- SKU name and part number;
- package width, height, and depth;
- packaged weight;
- rigid, flexible, or irregular packaging description;
- expected issues per day or week;
- desired replenishment interval;
- all physical variants and sizes;
- consumable or returnable status;
- required user-authentication method;
- required transaction fields;
- network environment;
- reporting and integration requirements;
- photos and physical samples for difficult products.
That information gives the manufacturer something concrete to engineer. “We need a tool vending machine for 30 items” does not.
Ask for a lane map, not just a cabinet drawing
A final proposal should show where the key SKUs will go and how much inventory each position can hold. That drawing exposes capacity problems early.
If the fast-moving abrasive has one shallow lane while a rarely used component occupies a large compartment, the problem is visible before production. The layout can be corrected before steel is cut or software is configured.
Separate published hardware capability from project capability
A base model may support a particular screen, network connection, or capacity. That does not mean every custom MRO function is included automatically.
Employee credential integration, role-based limits, work-order fields, asset returns, special reporting, or integration with another system should be confirmed in the project specification. The final quotation should state which functions are standard, which are configuration work, and which require development.
Pilot and Rollout Planning
One measured pilot usually teaches more than a broad first deployment.
The pilot should have a defined SKU group, user population, physical area, and baseline. Starting with “the whole storeroom” makes it difficult to determine which change produced which result.
Measure before the machine arrives
Record consumption for the products that will enter the machine. Measure retrieval time rather than guessing it. Record urgent purchases, stockouts, and inventory administration where those costs are relevant.
If production volume changes substantially from week to week, choose an activity measure that allows consumption to be normalized. A hundred insert packs during a high-output week may represent better performance than eighty packs during a slow week.
Use the first weeks to fix reliability
Do not focus on savings while employees are still reporting jams or authentication problems. First confirm that the physical system works.
Review failed vends, package movement, refill errors, connectivity, incorrect permissions, stock discrepancies, and user confusion. Fix mechanical and workflow problems before judging the economics.
Then tune capacity and rules
Once transactions are stable, the machine begins producing useful operating information.
A SKU that empties early needs more capacity or a different refill point. A product that barely moves may not deserve a lane. Repeated overrides may show that a quantity rule is unrealistic. A crowded interface may need fewer choices per screen.
The second machine should usually be better configured than the first one because the first machine has produced real usage data.
What would make me expand the program?
I would want to see four things.
- Reliable dispensing: the core SKU mix works without repeated intervention.
- Accurate records: physical stock and reported transactions are acceptably aligned.
- Operational acceptance: employees can obtain normal supplies without creating a new bottleneck.
- Financial evidence: measured benefits still support the project after recurring costs are included.
A pilot can still be successful even when it reveals that the original machine was wrong. Discovering that a locker is needed instead of a coil cabinet before purchasing ten units is valuable information.
Where a Tool Vending Program Usually Goes Wrong
Most weak deployments are not caused by one dramatic engineering failure. Small assumptions accumulate.
The machine is positioned where refill staff can reach it but technicians still have to walk too far. Fast-moving SKUs are given the same capacity as slow ones. Packaging is approved from dimensions without physical testing. Access limits are chosen before anyone measures actual usage. Reports are collected but nobody owns replenishment. Software fields are added because they are available, not because anyone needs them.
Each mistake looks minor. Together they can erase much of the value that justified the project.
A tool vending machine should therefore be treated as a small inventory system with mechanical dispensing, not as a cabinet purchase. Procurement, maintenance, operations, IT, safety, and purchasing may all have something useful to contribute, but each group should be involved only where its decisions affect the workflow.
The most practical design is usually the one that users barely notice. The item is close. The transaction is short. The package dispenses. The stock level is visible. Replenishment happens before the lane is empty. When something fails, the service path is obvious.
Final Buying Perspective
A tool vending project is ready to scale when the machine dispenses the real SKU mix reliably, refill labor is understood, transaction records are accurate, and the measured savings still support the investment after recurring costs are included.
Start with the product list rather than the cabinet catalog. Test difficult packages physically. Design capacity from the desired refill interval. Keep routine access simple. Treat returnable tools differently from consumables, and put the acceptance test in writing before shipment.
Zhongda Smart is worth evaluating early when the project needs a configurable industrial vending platform rather than a fixed retail layout. The reason is not a marketing label; it is the ability to work across different dispensing structures and adapt the cabinet, product channels, interface, connectivity, and remote-management configuration around the actual application.
Everything else is secondary to one question: does the finished system give employees reliable access while producing enough inventory control and measurable operating value to justify owning it?
Frequently Asked Questions
What is a tool vending machine?
A tool vending machine is a controlled self-service system used to issue tools, MRO supplies, PPE, maintenance parts, and other workplace inventory. A user authenticates, selects an approved item, and the system can record the issue and update inventory. Depending on the product, the machine may use spirals, pushers, lockers, drawers, or other dispensing mechanisms.
What items work best in an MRO vending machine?
Frequent-use, compact, easily packaged, or difficult-to-control items are usually the strongest candidates. Examples include cutting inserts, drill bits, blades, grinding discs, batteries, tapes, adhesives, fasteners, packaged PPE, fuses, filters, and small maintenance components. Large, fragile, irregular, or returnable items may need lockers or another controlled-access format.
Can a tool vending machine reduce MRO costs?
It can when the existing process contains measurable waste or friction. Potential benefits include shorter retrieval time, lower uncontrolled consumption, fewer manual issue tasks, better replenishment, fewer emergency purchases, and improved inventory visibility. The savings percentage should be calculated from the buyer's own baseline rather than assumed from a supplier claim.
How much does a tool vending machine cost?
There is no useful single price for a complete project because base cabinet cost and installed system cost are different. Hardware, dispensing configuration, user authentication, software, custom engineering, connectivity, freight, installation, commissioning, and spare parts can all affect the final amount. Published standard-machine prices are useful starting references, but a controlled MRO deployment should be quoted against the actual SKU and workflow requirements.
How do I calculate tool vending machine ROI?
Measure the present cost of retrieving supplies, controlled-item consumption, inventory administration, urgent purchasing, and any other benefit that can be supported with real records. Subtract recurring software, connectivity, refill, service, and maintenance costs. Simple payback is the installed project cost divided by monthly recurring net benefit. A break-even calculation can also show how much annual benefit the project must generate to meet a chosen payback target.
Should I choose a locker or coil vending machine for tools?
Coils are useful for stable packaged products that can move reliably through a lane and tolerate the delivery path. Lockers are usually a better starting point for irregular kits, larger products, fragile items, or tools that should be retrieved directly. Physical sample testing should confirm the choice because package behavior cannot be predicted from dimensions alone.
Can a vending machine track returnable tools?
Yes, but the required level of tracking matters. A locker can record which user opened a compartment. That does not necessarily identify which serialized asset was removed or returned. If individual asset identity matters, the system may need barcode, RFID, serialized scanning, or another item-level identification method in addition to controlled access.
How many SKUs should a tool vending machine hold?
The correct number depends on physical variants, product dimensions, issue volume, and refill frequency. A machine with many selections can still be undersized if fast-moving products have too little stock capacity. Calculate required inventory for important SKUs from average daily issues, planned days between refills, and an appropriate operating buffer.
What should I send a manufacturer before requesting a quote?
Send the SKU list, packaged dimensions, packaged weight, photographs, expected issue quantities, required refill interval, physical variants, consumable or returnable status, authentication method, reporting requirements, network conditions, and physical samples for unusual products. Better input produces a more useful lane design, capacity estimate, and quotation.
What should be tested before the machine ships?
Test the actual products from full, partial, and nearly empty lanes; confirm authorized and unauthorized access; demonstrate failed-vend handling; verify restart and network-loss behavior; check required reports; and test relevant lockers, doors, sensors, and inventory updates. The agreed results should be documented before the configuration is accepted.
How often does an industrial vending machine need maintenance?
There is no universal interval. Refill visits should include basic inspection, while cleaning, representative test vends, mechanical inspection, software checks, and deeper service should follow machine usage, operating conditions, fault history, and manufacturer instructions. Recurring failures should be investigated by product and lane instead of being treated as generic machine jams.
Is employee payment required for an MRO vending machine?
No. Workplace vending often uses the vending mechanism without a retail payment transaction. Employee credentials, PINs, cards, QR codes, or another approved identity method can be used to authorize an issue and assign consumption to a person, department, job, or cost center.
Sources and References
- Bureau of Labor Statistics. Employer costs per hour worked for private-industry manufacturing workers, June 2026. The cited chart reports $32.50 in wages and salaries and $16.12 in benefits per hour worked.
- Occupational Safety and Health Administration. 1910.132, General Requirements for Personal Protective Equipment, including employer payment provisions for required PPE subject to specified exceptions.
- Occupational Safety and Health Administration. 1910.147, Control of Hazardous Energy, used here as a reference for servicing and maintenance risk.
- National Institute of Standards and Technology. NISTIR 8259 Series, cybersecurity guidance for IoT product manufacturers and connected devices.
- Zhongda Smart. Current ZD-C-7, ZD-BGS-32, industrial vending, PPE vending, and OEM/ODM specifications referenced inline above. Product configurations and published reference prices should be reconfirmed when a project is quoted.
Disclaimer: This article is provided for equipment evaluation, procurement planning, and general operational information. It is not legal, safety, cybersecurity, accounting, engineering, or financial advice. Machine configuration, mounting, electrical work, network connection, PPE distribution, maintenance, repair, and energy-control procedures should follow applicable requirements, qualified-person practices, site risk assessments, manufacturer instructions, and the final contractual specification. Product specifications and published reference prices can change and should be reconfirmed before ordering. ROI examples are illustrative calculations. Actual cost, consumption, uptime, savings, labor impact, and payback depend on the specific products, workflow, machine configuration, operating conditions, software, and management process.